How to calculate your TRS and improve your industrial performance?
The Synthetic Yield Rate (the TRS) is the most widely used industrial performance indicator in production workshops. Yet in many factories, it remains poorly measured, poorly understood, or calculated too late to be truly useful.
A TRS calculated at the end of the week based on approximate manual inputs does not allow for the management of a production line. It can at most provide an indication of what has happened and build action plans to drive medium-term improvement.
In this article, we explain How to calculate your TRS correctly, what each component reveals about your actual performance, and how to turn this indicator into a concrete lever for improvement.
What is the TRS?
The Synthetic Return Rate (TRS), also known as OEE in English, for Overall Equipment Effectiveness, is an industrial performance indicator that measures’real efficiency of a production line.
It answers a simple question: about the time when your line was supposed to produce, What proportion was actually used effectively, at the right pace, in producing compliant parts?
The TRS is expressed as a percentage. The higher the value, the more efficient your line is. The lower the value, the more losses (in time, speed, or quality) that can be reduced.
It is the benchmark indicator of the continuous improvement approach in industry, particularly in the agro-food, pharmaceutical, plastic and mechanical sectors. It is complementary to the TRG (Total Return Goal), which also incorporates planned stops. The TRS remains the most frequently used indicator in day-to-day operations.
The TRS formula:
The TRS is calculated by multiplying three rates:
Each of these three factors measures a different dimension of your line's performance.
Availability
Availability measures the proportion of planned production time which was actually used to produce. It includes all the stops, planned or not, that prevented your line from operating.
The most common causes of degraded availability are:
- Unexpected machine breakdowns
- Lack of raw materials or operators
- Unplanned cleanings and maintenance
The performance
The performance measured the difference between the cadence at which your line actually produces and the cadence at which it should theoretically produce. It captures micro-stops, slowdowns and sub-rates, often invisible to the naked eye but very costly in the long run.
The most common causes of degraded performance:
- Unplanned micro-stops (less than a few minutes)
- Operators reduce cadence to avoid defects
- Outdated or poorly adjusted equipment
- Non-compliant raw materials slowing down production
The quality
Quality measures the proportion of conforming parts among all the parts produced. It includes rejects, rework, and non-conformities, in other words, everything that has been produced but cannot be delivered as-is.
The most common causes of degraded quality are:
- Machine adjustment deviations
- Raw materials not specified
- Defects at the beginning or end of the series
- Uncontrolled processes
Example of TRS calculation:
Let's take a concrete example with an food production line.
Line data:
- Expected opening time: 8 hours (480 minutes)
- Actual production time: 360 minutes (stops: 120 minutes)
- Theoretical speed: 100 pieces/hour
- Actual observed cadence: 80 pieces/hour
- Number of parts produced: 480 parts
- Compliant parts: 456 parts
Calculation:
Availability = 360 ÷ 480 = 0.75, that is 75%
Performance = 80 ÷ 100 = 0.80, that is 80%
Quality = 456 ÷ 480 = 0.95, that is 95%
TRS = 0.75 × 0.80 × 0.95 = 0.57, that is 57%
This result means that over the planned production time, only 57% was actually used effectively. The remaining 43% represent losses in availability, performance or quality that can be addressed.
What this calculation reveals: The most penalizing factor here is availability (75%). This is where the improvement actions will have the strongest impact. By raising the availability to 90% and keeping the other factors constant, the TRS would increase to 68,4%, That is +11 points, only by reducing downtime.
The 5 most common causes of a low TRS
In our experience with more than 130 industrial sites, these five factors account for the majority of disappointing TRS results.
1. Unplanned stops
These are the most insidious losses. A 3-minute pause that repeats 20 times per shift represents an hour of production lost — never clearly shown in the reports. These micro-stops are only visible with a system for automatically collecting data.
3. Mismanaged series changes
Each change in a series is a source of loss of availability. Without a structured method (such as SMED) and without reliable data on the actual times of changes, these losses remain difficult to reduce.
2. The rhythm is not kept without an identified reason
Operators sometimes adjust the cadence below the theoretical one without documenting the reason. Over time, these adjustments represent significant performance losses — and impossible to correct if they are not seen.
4. Reactive maintenance rather than preventive maintenance
A line that fails due to lack of preventive maintenance generates unplanned, long and costly outages. The link between preventive maintenance and TRS availability is direct and often underestimated.
5. Inaccurate data
Finally, a TRS calculated based on manual inputs or end-of-service estimates is simply not reliable. It may appear good — or bad — without reflecting the reality on the ground. Making improvement decisions based on approximate data is like driving blindly.
How to improve your TRS? The 3 levers that can be taken action on
Lever 1: measure continuously, not at the end of the shift
The first condition for improving your TRS is to measure it accurately, in real time. A TRS calculated once a week using paper sheets does not allow you to identify the causes of loss at the right time.
TRS monitoring software connected directly to your lines via sensors, automation, or the OPC-UA protocol collects the data automatically and displays the TRS minute by minute. It is this granularity that allows for immediate action, rather than having to detect losses afterwards.
Lever 2: Identify and prioritize the causes of loss
Once the data have been collected reliably, the next step is to classify the causes of loss by frequency and impact. Not all causes deserve the same attention; some rare but long stops have more impact than a multitude of short micro-stops.
The Pareto analysis of the causes of loss allows for the focus of continuous improvement efforts on the 20% causes that generate 80% of TRS losses.
Lever 3: Involve the field teams
Improving TRS cannot be achieved without the operators. They are the ones who know the true causes of downtime, the adjustments in rhythm and the quality deviations. A visual management tool accessible in the workshop, which displays the TRS in real time on an online screen, naturally involves the teams in the performance process.
When an operator sees their TRS drop in real time, they understand the impact of each stoppage and become an active participant in the improvement rather than just a simple executor.
Estimate the financial impact of improving your TRS
A TRS gain is concrete and quantifiable. Here are some order of magnitude figures.
On a production line 3,000 pieces per day, with a selling price of 10€ and a net margin of 10% :
- 1 TRS point won ≈ 9,000€ per year
- 5 TRS points won ≈ 45,000€ per year
- 10 TRS points won ≈ 90,000€ per year
These figures vary depending on your selling price, margin and production volume. To obtain a personalized estimate in 2 minutes, use our productivity gain calculator.
TRS, TRG: what difference does it make?
The TRS is not the only indicator of industrial performance. It is often used in conjunction with the TRG.
The TRG (Total Return Rate) It integrates planned outages (series changes, cleanups, scheduled maintenance) into the calculation. It provides a more comprehensive view of all losses, including those that are accepted as inevitable. The difference between TRS and TRG assesses the organizational loss of your site.
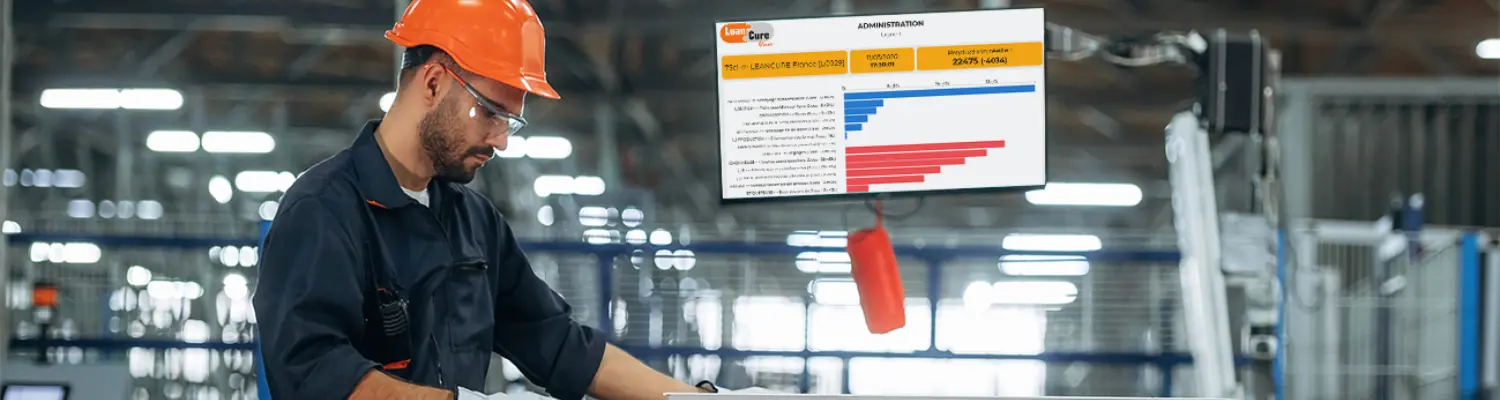
The two indicators are complementary and can be monitored using Leancure View MES.
How Leancure View automates the calculation and tracking of your TRS
Calculating your TRS manually from sheet records is possible — but it is a source of errors, delays, and unreliable data. And above all, a TRS calculated at the end of the shift arrives too late to correct deviations in real time.
Leancure View MES automates the entire process:
- Automatic collection stop times, rates and quantities produced: directly from your equipment via sensors, automation or the OPC-UA protocol
- Real-time TRS calculation, minute by minute, line by line, without manual input
- Display in the workshop on a tablet or dynamic screen, to involve field teams in the performance process
- Analysis of the causes of loss classified by frequency and impact to prioritize actions
- Automatic reports generated in one click, exportable, without data manipulation
The installation takes place in one day on your existing lines. The first data arrives the next day. The first TRS gains are measurable within a few weeks.
The TRS is an indicator simple in its formula: Availability × Performance × Quality, but powerful in what it reveals about the real efficiency of your production lines.
Calculating it correctly is the first step. Measuring continuously and in real time This is what really enables us to act on the right causes at the right time, with the greatest impact.
A gain of 5 TRS points represents several tens of thousands of euros saved each year, on the lines you already have, without additional physical investment.
 Français
 English
 Türkçe
 Polski
 Español
 العربية
 Italiano